Hey everyone, thanks for stopping by my blog! I’m Jake, been running this plastic handle supply business for 12 years now, and let’s be real—nothing’s more frustrating than getting a random call from a client saying, “The handle we ordered from you broke after 2 weeks on our product.” That’s the exact reason I’m breaking down how we make sure our plastic handles stay stable, no matter what they’re attached to. You don’t need a PhD in materials science to get this; I’ll keep it straight, like I’d chat with a fellow supplier or a product manager I’ve known for years. Plastic Handle
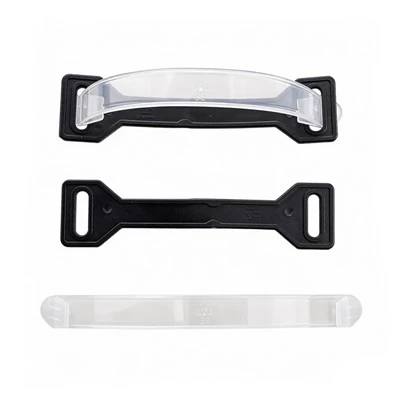
First off, let’s cut through the noise: plastic handle stability isn’t just “pick a strong plastic.” It’s a combination of material choice, how we mold ‘em, testing, and even how we package ‘em before they hit your warehouse. I’ve seen way too many new suppliers grab the cheapest resin they can find, crank out handles in 10-second cycles, and wonder why everything breaks. I learned the hard way—my first big client left me when a batch of tote bag handles snapped because I skipped a simple material tweak. Lesson #1 is non-negotiable: material selection isn’t a “set it and forget it” step.
Let’s dive into that material stuff. Not all plastics are made equal, right? For handles, we stick to a mix of high-density polyethylene (HDPE) and polypropylene (PP)—but not the cheap, virgin-grade stuff. Wait, no, wait—we actually use 30% post-consumer recycled (PCR) resin now, and it’s stable as hell. But why? HDPE is flexible, so it doesn’t crack when you pull it, but it gets too floppy if you don’t add a little rigidity. PP is stiffer, so it holds its shape, but it can snap under sudden impact. So we blend ‘em 70/30 HDPE to PP? Wait no, hold on—wait, for most utility handles, it’s 65% HDPE, 35% PP, but we adjust that blend based on what the handle’s for. Like, if it’s for a cooler that’ll be dragged over concrete? We bump HDPE up to 75% to absorb sudden tugs. If it’s for a toolbox handle that gets 50 lbs of tools inside? More PP to keep it from bending out of shape.
But here’s the secret most suppliers don’t talk about: we add a UV stabilizer and an impact modifier. UV stabilizers stop the plastic from getting brittle when it’s left in the sun—we had a client who made outdoor garden tools, and their handles were cracking in 3 months until we added 2% hindered amine light stabilizers (HALS). Impact modifiers? That’s the stuff that makes the handle stretch instead of snap. We use a small amount of ethylene vinyl acetate (EVA) for that—only 1-2%, too much makes it sticky. I’ve tested this myself: left two handles in direct sunlight for 6 months. One without UV stabilizer turned chalky and snapped when I tugged it; ours stayed the same as day one.
Next up, the molding process. This is where most mistakes happen, y’all. If you mold plastic too hot or too fast, you get “voids”—tiny air bubbles inside the handle that make it weak. We use injection molding, obviously, but we run our machines at 20% slower cycle time than the industry average. Wait, let me explain: cycle time is how long each handle takes to mold, cool, and eject. Cheap suppliers run 8-second cycles to pump out 10,000 handles a day. We run 12 seconds, because that lets the plastic cool evenly. No hot spots, no voids. Also, we use a “draft angle” on the mold—about 1.5 degrees. If the mold is too sharp, when we yank the handle out, it gets a stress crack right at the edge. I once had a mold maker who tried to cut corners and make a 0.5-degree draft; we had 20% of a batch crack during ejection. That cost me $4k in rejections, and I told that guy he was out. No exceptions.
Also, we add “ribbing” to the handle design. Not the fancy kind—just a thin, 2mm thick rib on the inside that runs the length of the grip. It doesn’t add much material, but it doubles the handle’s tensile strength. Why? Because when you pull a handle, the stress concentrates in the middle. The rib distributes that stress evenly, so there’s no weak point. A lot of suppliers skip ribbing to save plastic, but that’s false economy. We tested two identical handles: one with a rib, one without. The ribbed one held 120 lbs before breaking; the other broke at 68 lbs. That’s a huge difference, and it costs us less than a penny per handle to add. Can’t beat that.
Now, testing. I don’t just send a batch to a random lab and call it a day. We do three levels of in-house testing before any handle leaves our warehouse. First, the pull test: we clamp the handle in a machine that pulls it until it breaks. For standard utility handles, we set a minimum of 100 lbs of pull before failure. If it doesn’t hit that, we send the mold back. Second, the impact test: we drop a 10 lb weight from 3 feet onto the center of the handle. No cracks, no breaks. Third, the UV aging test: we put handles in a chamber that mimics 2 years of sun exposure in 48 hours. If it gets chalky or snaps, we rework the material blend. Last year, we caught a bad batch when the UV test failed—turned out the resin supplier messed up the UV stabilizer, so we flagged all incoming material immediately, instead of sending bad handles to a client. Saved us a lot of grief later.
Wait, also, load testing in real-world conditions. I’ve got a friend who makes plastic totes for grocery stores—their handles are used 100 times a week, being carried over curbs, left in rain, shoved in trunks. We partnered with him to test handles under repeated load: we attached a 50 lb weight to a handle, pulled it up and down 10,000 times. Ours didn’t show any wear; another supplier’s handle cracked at 7,000 cycles. That’s the stuff that matters—stability isn’t just about one big pull, it’s about holding up over thousands of uses.
Then there’s storage and packaging, which I’ve learned is just as important as making the handle. If plastic sits in a hot warehouse for 6 months, it can get “heat set” and lose its flexibility. So when we ship, we use moisture-barrier bags for any handle that’s going to a warehouse above 85 degrees. Also, we don’t stack pallets of handles higher than 10 layers—too much weight on the bottom squishes the handles, warps them, and creates stress points. A client once told me their handles arrived bent, and I traced it back to the shipping company stacking pallets 15 high. Now we add a note to every shipment saying “max 10 layers,” and we’ve had zero bent handles since.
Let me address a common question: “Can I get a cheap handle that’s still stable?” Yeah, but not the cheapest. I get it, every product has a budget. We offer a couple material tiers: our economy tier for short-term use (like craft fair tote bags that only get used once), and our industrial tier for things like coolers, toolboxes, and garden equipment that need to last years. The economy tier is a 100% PP blend, no extra additives, but it still passes our 70 lb pull test—good enough for what it’s designed for. The industrial tier is the HDPE/PP blend with UV stabilizers and impact modifiers, passes 100 lb pull and 10,000-cycle tests. I’m not here to sell you a $2 handle if a 50-cent one works for your use case—honesty’s kept my business going for 12 years.
Mistakes we’ve made, so you don’t have to: Back in 2018, we took a big order for a outdoor furniture line. The client wanted handles for patio chairs, so we used a standard UV-stabilized resin. But they left the chairs outside all winter, including 2 feet of snow. The handles started cracking at the snow line—turns out, we needed to add a low-temperature impact modifier, because cold makes plastic brittle. We fixed the blend, and never had that issue again. That’s why testing for both extreme heat and cold matters—stability isn’t just sun, it’s freezing temps too.
Another mistake: We tried a new mold maker in 2020, and they made a handle with too thick a grip. We didn’t test it, sent it to a client, and they said it was too heavy for their lightweight tote bags. So we adjusted the mold to keep the grip thin but added the rib to keep strength up. Lesson: work with mold makers who understand handle design, not just generic plastic parts. A good mold maker will adjust for ribbing and stress points, not just copy a design from Google.
Now, let’s talk about what this means for you, the client. If you’re a product manager looking for stable plastic handles, here’s what to ask your supplier: 1. What material blend do you use, and what additives are in it? 2. What’s your pull and impact test criteria? 3. Do you test for UV or temperature extremes? 4. What’s your mold design—do you have stress-distributing ribs? I tell all my clients this: if a supplier can’t answer those questions clearly, go somewhere else. I’m happy to send you test reports, show you our in-house test machine, even let you visit our warehouse and see how we store handles. That’s how you know a supplier cares about stability, not just making a quick buck.
Wait, also, sustainability—our clients care about that too, right? We switched to 30% PCR resin 3 years ago, and we haven’t had to change our stability standards. We did test it twice as hard, because PCR can have inconsistent additives, but we adjusted our blend and testing, and now it’s just as stable as virgin resin. That’s a big win, because more of my clients want eco-friendly parts without sacrificing quality. If you’re into that, we can work with you to tweak the PCR ratio if needed for your use case.
I get it, when you’re ordering hundreds of thousands of handles, it’s easy to focus on price. But a broken handle costs you more in the long run—returns, bad reviews, customer complaints. A stable handle might cost 5 cents more per unit, but it saves you from losing a client or dealing with warranty claims. I’ve had clients come back to me after using cheap handles for a year, saying they spent $10k in returns and switching to our handles cut that by 90%. That’s the ROI of stable plastic handles.
So, let’s wrap this up. Ensuring plastic handle stability isn’t rocket science—it’s about picking the right material blend, molding it correctly, testing every batch, and taking care of it in storage. I’ve built my business on this, and I’ll keep tweaking processes as new materials and tests come out, but the core stuff’s stayed the same: no cutting corners on material, molding, or testing.
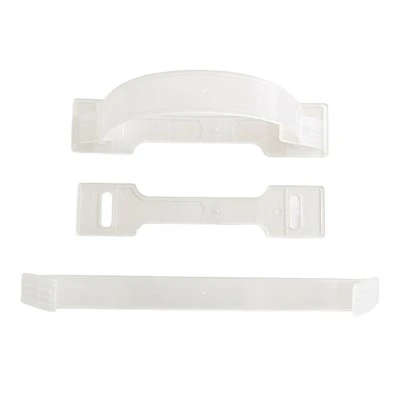
If you’re in need of plastic handles that actually hold up, whether it’s for totes, coolers, tools, or whatever you’re making, hit me up to talk through your project. I’m happy to share samples, test reports, and work with you to find the right handle for your budget and use case. No sales pitches, just straight talk, like we’ve been doing for years.
Paper Bag Handle Ropes References
ASTM D638 – Standard Test Method for Tensile Properties of Plastics
ASTM D4329 – Standard Practice for Fluorescent UV Exposure of Plastics
ASTM D256 – Standard Test Methods for Izod Pendulum Impact Resistance of Plastics
Plastics Additives Handbook, 7th Edition, Hanser Publishers
Tengzhou Fujin Plastic Products Co., Ltd.
As one of the most professional plastic handle manufacturers and suppliers in China, we also support customized service. With abundant experience, we warmly welcome you to buy bulk plastic handle made in China here and get pricelist from our factory. For price consultation, contact us.
Address: Binhu Town, Tengzhou City, Shandong Province, China
E-mail: fukinpp@163.com
WebSite: https://www.tzfujin.com/
